Mobile welding · AWS D1.1
Structural Welding & Steel Repair
Cracked, fatigued and failed steel repaired where it sits. Cracks are excavated to sound metal, rebuilt and reinforced, then documented at closeout.
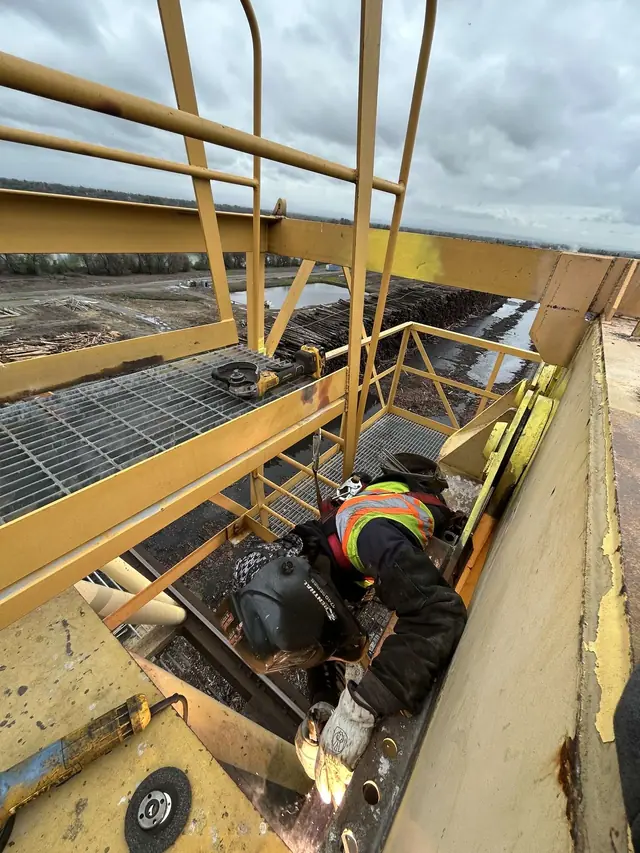
AHT performs structural welding on equipment frames, machine bases, fabricated steel assemblies and heavy attachments across twelve Northern California counties. Every repair starts with finding the full extent of the crack and ends with a documented weld.
Welding is performed to AWS D1.1 under written welding procedure specifications. Qualification records and weld documentation are available on request, so the work holds up to an inspector as well as to the load.
What AHT handles
- Crack excavation to sound metal and full-penetration repair
- Reinforcement plates, gussets and doublers
- Weld restoration on fatigued and failed joints
- Multi-pass welding on heavy sections, 1 in. and up
- Repair and reinforcement of fabricated steel assemblies
- Weld documentation where the job requires it
Equipment
- Equipment frames and subframes
- Machine bases and skids
- Booms, arms and attachments
- Truck and trailer frames
- Conveyor and plant steel
- Tanks, hoppers and chutes
Where structural repair is needed
Structural welding at AHT covers steel that carries load: equipment frames and subframes, machine bases and skids, booms and attachments, truck and trailer frames, and conveyor and plant steel. The common thread is a joint that has cracked, bent or worn past the point where it carries its load as designed.
Each repair is scoped in writing before work starts. The scope states what is cracked, what is removed and rebuilt, and what reinforcement is added, so the price and the finished repair match.
Why repaired steel cracks again, and how AHT prevents it
Most repeat failures come from a repair that covered the crack instead of removing it, or from a joint that was never designed for the load it now carries. A bead laid over a crack leaves the crack underneath, and it grows back through the new weld.
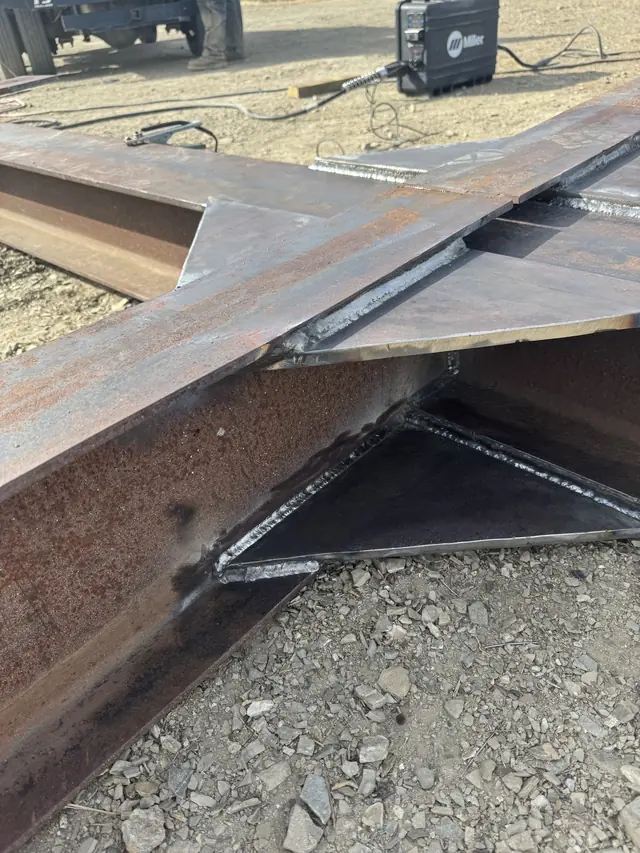
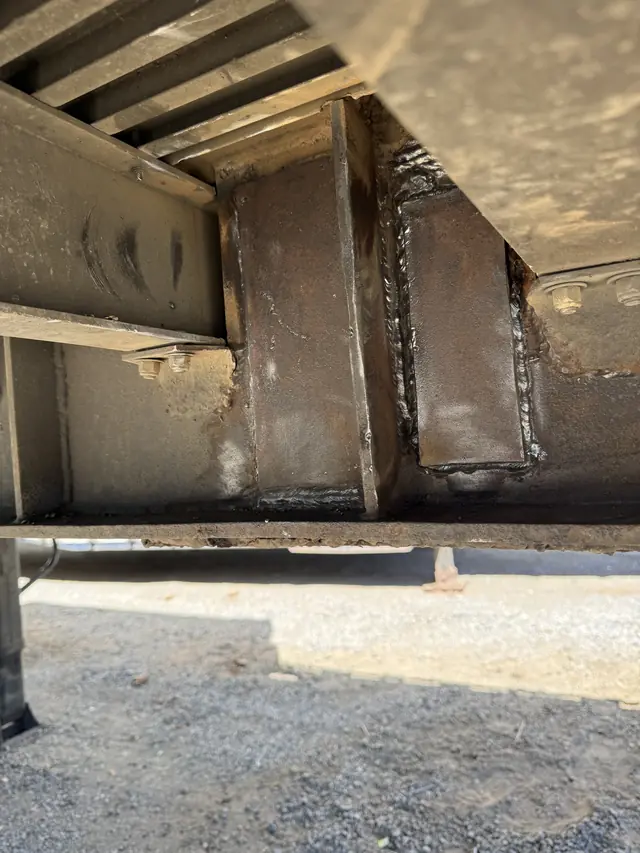
AHT excavates each crack to sound metal, drills the ends, and rebuilds the joint to full section. Where the load path is the problem, reinforcement plates, gussets or doublers spread the stress so the repaired area is no longer the weak point.
Signs a joint needs attention
- Rust bleeding from a weld toe, or a fine line through the paint
- A crack that was welded over before and has come back
- Movement, flex or noise at a joint under load
- Bent or distorted members after an impact or overload
- Broken welds at gussets, brackets and mounts
Procedures and documentation
- Welding to AWS D1.1 under written welding procedure specifications
- Stick (SMAW) and flux-cored (FCAW) processes, chosen for the steel and the site
- Preheat and interpass control where the procedure requires it
- Visual inspection of every completed weld
- Photo documentation and a written closeout for every job
- Welder qualification records available on request
In the field
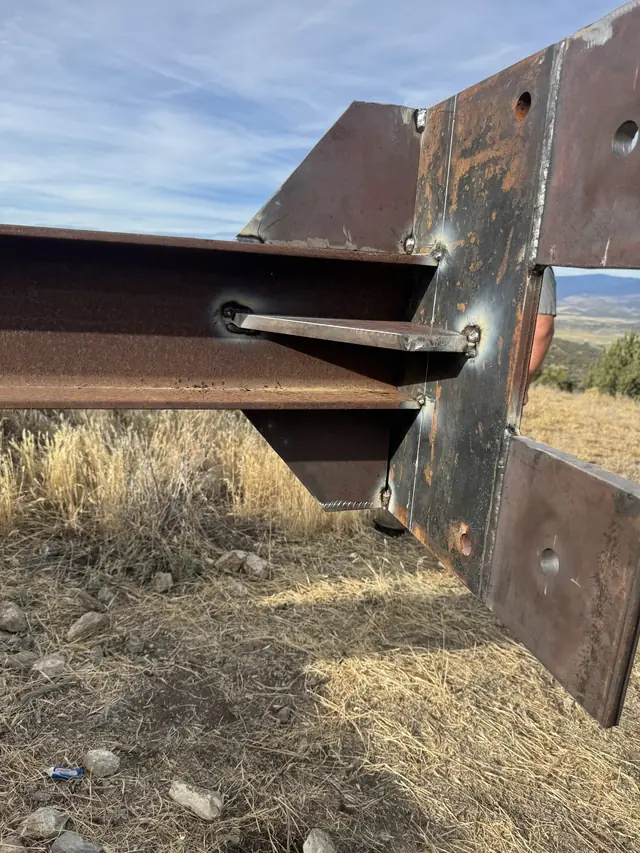
Is structural welding done on site?
Yes. AHT mobilizes a self-contained rig with on-board generator power, so repairs are made where the equipment or assembly sits.
What documentation comes with a structural repair?
A written scope before work starts and a signed completion record at closeout. Welding procedure specifications and welder qualification records are available on request.
Can AHT fabricate the reinforcement on site?
Yes. Plates, gussets, doublers and brackets are cut, fitted and welded on site as part of the repair.
Can a cracked frame be repaired instead of replaced?
In most cases, yes. A crack excavated to sound metal, rebuilt to full section and reinforced where the load path requires it restores the frame without the cost and lead time of a replacement. The written scope states plainly when replacement is the better option.
What thickness and positions can AHT weld?
Welder qualifications cover AWS D1.1 in 7018 stick and flux-core, self-shielded and gas-shielded, all positions, unlimited thickness. Heavy sections are welded in multiple passes with preheat and interpass control where the procedure requires it.
Related
Related services.
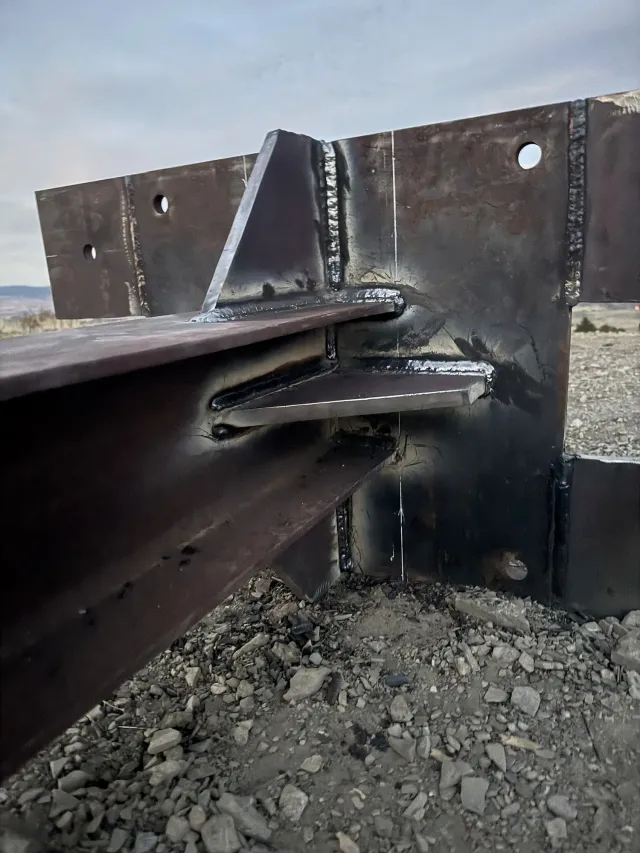
Field & Custom Fabrication
Custom and field fabrication: plates, brackets, mounts, guards and replacement members built to fit.
Learn more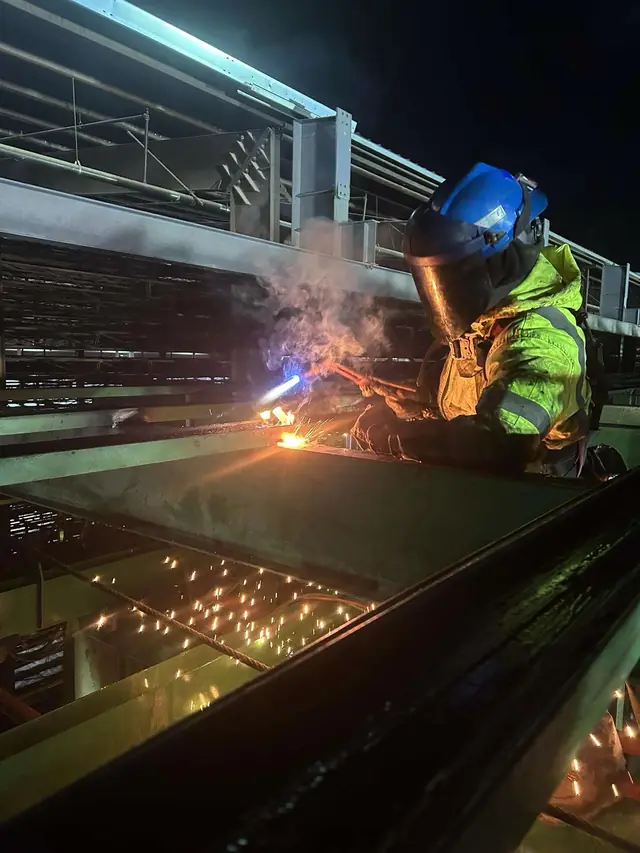
On-Site Cutting & Gouging
Torch cutting and carbon arc gouging to remove failed welds and prepare joints.
Learn more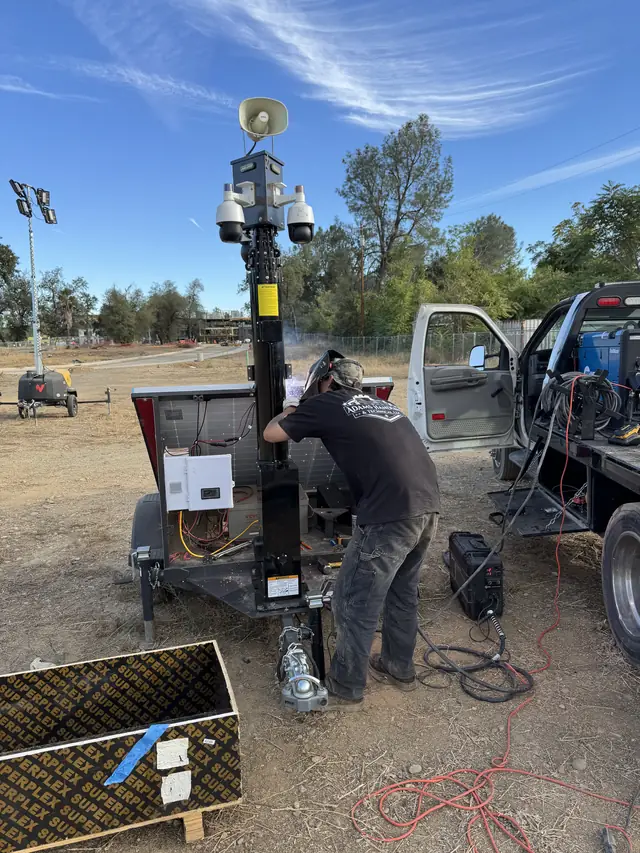
Trailer & Truck Frame Repair
Cracked I-beams, crossmembers, spring hangers and underride guards repaired on site.
Learn moreRequest service
Cracked or failed steel?
Call AHT or send photos. The repair is scoped in writing before any work starts.